How to Choose Crown Block Components for Global Procurement?

Time:2026-10-12 Author:Charlotte
0%

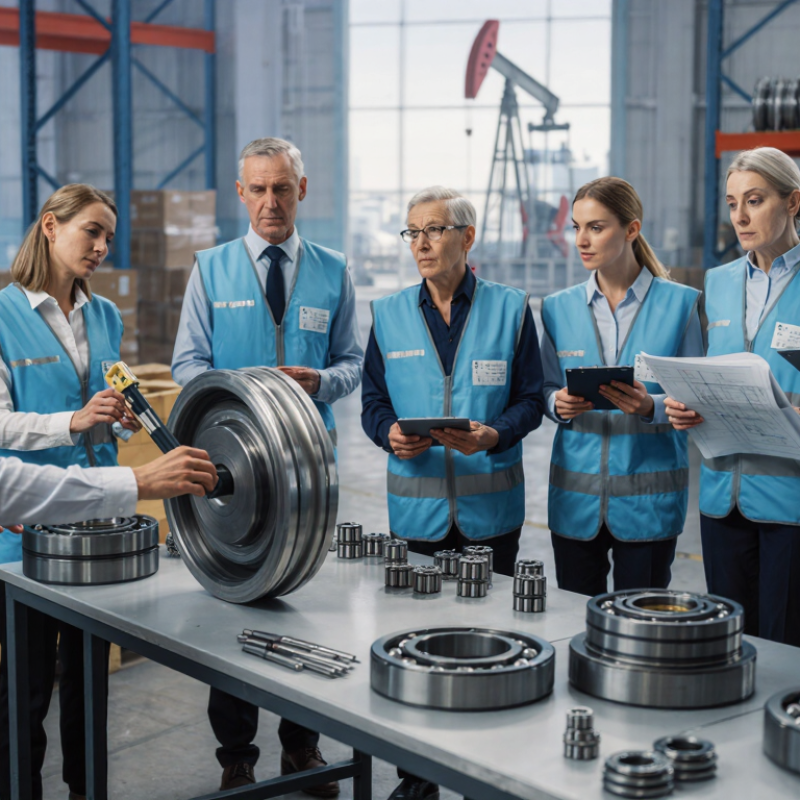
Global procurement of Crown Block Components demands more than comparing unit prices. It requires evidence, engineering judgment, and disciplined supplier verification. The IEA’s Oil 2024 report projects continued oil demand growth through 2025, while Baker Hughes’ International Rig Count tracks ongoing drilling activity across major regions. These indicators suggest sustained demand for reliable lifting equipment and replacement parts.

Small failures matter.

A worn sheave bearing can create vibration, heat, and unplanned downtime. A poorly matched pin may compromise load transfer. Procurement teams should therefore examine rated capacity, sheave diameter, bearing design, material certificates, heat treatment, lubrication access, and dimensional compatibility. API Specification 8C provides an important reference for drilling and production hoisting equipment. It should support, not replace, project-specific engineering review.

Supplier quality systems deserve equal attention. Request inspection plans, factory acceptance records, non-destructive testing results, traceability documents, and realistic lead times. Confirm whether the manufacturer can support installation guidance and replacement parts near the operating region. Deloitte’s 2024 Oil and Gas Industry Outlook highlights cost discipline and supply-chain resilience as continuing industry priorities. That context makes lifecycle value more useful than the lowest quotation.

No spreadsheet sees everything.

A supplier may offer excellent documents but weak field support. Another may have strong experience but limited production capacity. This guide examines how to balance technical performance, certification, delivery risk, maintenance access, and total ownership cost when selecting Crown Block Components. Procurement plans are rarely perfect. Careful questions, documented assumptions, and independent inspection can make them considerably safer and more dependable.
How to Choose Crown Block Components for Global Procurement?

Define Crown Block Components and Their Procurement Requirements

How to Choose Crown Block Components for Global Procurement?

Crown block components include the frame, sheaves, shafts, bearings, guards, lubrication points, and load-monitoring devices. Their procurement requirements must begin with the rig’s actual working load, drilling line diameter, sheave groove profile, and operating environment. API Specification 8C provides a recognized basis for design, inspection, and rated-load verification. Procurement teams should request load charts, material certificates, heat-treatment records, nondestructive testing results, and dimensional drawings. Small errors matter. A groove that does not match the drilling line can accelerate wear and create uneven loading.

Global demand also affects purchasing decisions. The International Energy Agency’s Oil 2024 report projected oil demand to reach 106.1 million barrels per day by 2029. This outlook does not guarantee every rig project, but it supports careful planning for replacement equipment and critical spares. The Energy Institute Statistical Review 2024 reported global oil production of about 96 million barrels per day in 2023. That scale shows why supply continuity matters. Buyers should compare manufacturing lead time, corrosion protection, export packaging, warranty response, and local technical support. Factory acceptance testing should confirm rotation, runout, bearing temperature, braking interfaces, and emergency access. Photographs help, but they are not enough.

A spreadsheet can still miss field reality. Shaft journals may be worn, and older frames may contain undocumented modifications. I have seen procurement teams specify a rated load without checking the complete load path. That is a costly weakness. Require a site survey, verified interface dimensions, traceable serial records, and a spare-parts list before issuing the purchase order.

How to Choose Crown Block Components for Global Procurement?

Crown block components should be selected according to load capacity, compatibility, inspection requirements, operating conditions, and lifecycle support. The chart presents a practical evaluation-weight model for comparing suppliers without relying on company or brand data.

Procurement priorities should be verified against the drilling program, rated load, wire-rope size, sheave groove profile, applicable API requirements, environmental conditions, documentation, and available spare parts. The percentages are a planning benchmark for supplier evaluation and should be adjusted to the project specification.

Assess Load Capacity, Compatibility, and Operating Conditions

How to Choose Crown Block Components for Global Procurement?

A practical procurement review starts with load capacity, not price. Confirm the maximum static and dynamic loads, including shock loads during tripping operations. Check the crown block’s rated capacity against the complete assembly, not one isolated component. Sheave diameter must suit the wire rope diameter and construction. A mismatch can increase bending fatigue, rope wear, and heat. Bearing selection also matters under continuous rotation and changing loads. Request traceable material records, dimensional drawings, load-test results, and inspection reports from qualified suppliers. These documents support reliable technical decisions across different procurement regions.

Compatibility is equally important. Verify mounting dimensions, shaft sizes, rope grooves, lubrication points, and connection hardware before approval. Operating conditions may include dust, salt air, freezing temperatures, or high humidity. Seals, coatings, and lubricants should match those conditions. Do not assume a component rated for one rig will fit another. Small differences can stop installation. Field feedback is useful, but it is not always complete. A spreadsheet may look accurate while missing actual rope tension or maintenance history. That deserves a second review.

Tips: Build a comparison sheet with load, rope size, temperature range, corrosion exposure, and service hours. Ask suppliers to identify exclusions and uncertain data. Keep critical measurements in millimeters and use one consistent load unit. If operating conditions are unclear, specify conservative assumptions and confirm them with the site team. Recheck the final selection with an independent engineer before purchase.

Compare Materials, Manufacturing Standards, and Supplier Qualifications

Selecting crown block components for global procurement requires more than comparing quoted prices. Materials must match load, speed, corrosion exposure, and service temperature. Sheaves commonly use forged or cast alloy steel, while shafts need verified strength and accurate heat treatment. Bearings should suit the expected radial and axial loads. Small differences matter.

Manufacturing standards create a common technical language. Request documented compliance with applicable lifting equipment standards, controlled welding procedures, dimensional inspection, and non-destructive testing. Check groove profiles, shaft runout, bearing fits, and guarding details. Material certificates should link directly to component serial numbers. Load testing must reflect the intended duty, not only a convenient factory setup. ISO-based quality systems help, but certification alone proves little.

Supplier qualification should combine paperwork with technical evidence. Review production capacity, calibration records, inspection plans, and corrective-action history. Ask for sample inspection reports and traceability records before placing a large order. An independent factory audit can reveal poor storage, mixed materials, or unclear revision control. Communication also deserves attention. Can the supplier explain a tolerance without hiding behind technical language?

No checklist is perfect. A low-risk component may still cause delays when drawings, customs documents, or regional standards conflict. I would leave room for a technical review after the first production sample. That extra step costs time, but it can expose assumptions before they become expensive field problems.

Verify Inspection, Certification, and International Compliance

How to Choose Crown Block Components for Global Procurement?

When sourcing crown block components across borders, inspection should begin before price comparison. Request drawings, load ratings, material grades, and the operating environment. These details define what inspectors must verify. Check sheave groove profiles, bearing clearances, pin diameters, guards, and connection points. Ask for material certificates with matching heat numbers. Small gaps matter.

A certificate alone does not prove compliance. Confirm the issuing body, certificate scope, inspection date, applicable standard, and component serial number. An independent inspector should witness dimensional checks, surface examinations, hardness testing, and proof-load testing when required. Inspection photographs should show calibrated instruments and visible identification marks. Paperwork can mislead.

For international procurement, compare the supplier’s documents with destination-country rules and project specifications. Verify required conformity declarations, test reports, packaging labels, operating manuals, and traceability records. Translate critical documents accurately, not casually. I have seen acceptable components delayed because certificates used an outdated standard edition. That mistake is avoidable, but busy teams still make it. Keep a document register linking every component to its report, shipment, and inspection result. If a requirement is unclear, pause and obtain written clarification from a qualified compliance professional.

How to Choose Crown Block Components for Global Procurement? - Verify Inspection, Certification, and International Compliance

Component Primary Function Inspection and Test Requirements Typical Certification Evidence International Compliance Considerations Procurement Documents to Request Recommended Acceptance Criteria
Sheaves and Grooves Guide and support the drilling line while transferring load through the crown block. Dimensional inspection of pitch diameter, groove profile, flange height and rim thickness.
Visual examination for cracks, deformation and excessive wear.
Non-destructive testing of critical areas using magnetic particle or penetrant testing where applicable.
Material certificate EN 10204 3.1 NDT report Dimensional report Load-test record Confirm design and manufacturing requirements against API Spec 8C or the project specification.
Verify compatibility with the specified drilling-line diameter and reeving arrangement.
Approved drawings
Material heat numbers
Heat-treatment records
Inspection and test plan
Traceability matrix
All dimensions must match the approved drawing.
No rejectable indications in critical load-bearing zones.
Surface finish and groove geometry must be suitable for the specified line size.
Sheave Bearings Allow low-friction rotation of each sheave under radial and operational loads. Check bearing identification, internal clearance, seal condition and mounting fit.
Verify grease compatibility and lubrication condition.
Conduct rotation, noise and temperature checks during functional testing.
Certificate of conformity Material declaration Dimensional report Lubricant data sheet Confirm the bearing duty rating is suitable for calculated radial, axial and shock loads.
If supplied with electrical monitoring devices, assess the applicable hazardous-area requirements separately.
Bearing load calculations
Installation instructions
Lubrication schedule
Functional test report
Storage requirements
Correct fit and clearance without binding.
Smooth rotation with no abnormal noise, vibration or leakage.
Grease and seals must be suitable for the operating temperature range.
Main Frame and Side Plates Support sheaves, bearings and associated loads while maintaining structural alignment. Review welding procedures and welder qualifications.
Visual and dimensional inspection of welds and alignment.
NDT of specified welds using ultrasonic, magnetic particle or penetrant methods.
Welding procedure records Welder qualification records NDT reports Material certificate EN 10204 3.1 Apply the governing lifting-equipment standard and purchaser specification consistently.
Welding inspection personnel should be qualified under a recognized personnel-qualification scheme such as ISO 9712.
Certified fabrication drawings
Weld map
Weld repair log
Coating inspection report
Structural calculation summary
No unacceptable weld discontinuities.
Frame dimensions and sheave alignment must be within drawing tolerances.
Coating thickness and surface preparation must meet the project corrosion-protection specification.
Main Shafts, Pins and Retainers Carry concentrated loads and secure sheaves, bearings and other rotating assemblies. Verify diameter, straightness, keyways, threads and retaining features.
Check heat treatment and hardness where specified.
Perform surface NDT on fillets, shoulders, threads and other stress-concentration areas.
Material certificate EN 10204 3.1 Hardness report Heat-treatment record NDT report Confirm material grade, design factor and fatigue requirements from the approved engineering basis.
Ensure traceability is maintained from raw material to finished part.
Material traceability records
Machining inspection report
Heat-treatment chart
NDT procedure and results
Assembly instructions
No cracks or relevant linear indications.
Dimensions, hardness and surface condition must meet the approved specification.
Retaining devices must be positively secured and independently inspectable.
Guards, Covers and Access Platforms Protect personnel from moving parts and provide safe access for inspection and maintenance. Check guard openings, handrails, toe boards, walkways, fasteners and access clearances.
Verify that removable guards are securely retained and cannot contact rotating parts.
Dimensional inspection report Functional safety checklist Coating report Assembly certificate Design should satisfy applicable machinery-safety, workplace-access and lifting-equipment requirements in the destination jurisdiction.
Local requirements may apply to platforms, ladders, fall protection and restricted access.
Guarding drawings
Access and maintenance study
Fastener list
Risk-assessment extract
Installation instructions
No exposed hazardous nip points during normal operation.
Safe access to lubrication and inspection points.
Guards must not obstruct required maintenance or emergency procedures.
Lubrication System and Fittings Deliver lubricant to bearings and other service points to control friction, wear and corrosion. Verify fitting type, thread size, hose routing, pressure rating and accessibility.
Conduct leakage and pressure checks where a centralized lubrication system is supplied.
Pressure-test report Material declaration Lubricant compatibility statement Assembly checklist Materials and seals must be compatible with the specified lubricant and ambient conditions.
Any supplied electrical pump, sensor or control device may require separate conformity assessment.
Lubrication schematic
Hose and fitting specifications
Recommended lubricant data
Maintenance interval schedule
Spare-parts list
No leakage at operating pressure.
All lubrication points must be reachable and clearly identified.
Lubricant recommendations must include temperature and compatibility limits.
Fasteners and Locking Devices Secure structural, bearing and guard assemblies against loosening under vibration and cyclic loading. Verify grade, size, thread form, surface treatment and locking method.
Check tightening torque or tensioning records for critical connections.
Fastener certificate Coating certificate Torque record Traceability record Use the fastener standard specified by the engineering design, such as ISO metric fastener requirements where applicable.
Do not substitute grades or coatings without engineering approval.
Fastener schedule
Certificates of conformity
Torque procedure
Lot traceability
Approved substitution list
Correct grade and lot identification.
No damaged threads, corrosion or coating defects.
Critical joints must have documented tightening or tensioning results.
Crown Block Assembly Integrate the load-bearing components into a complete, tested and serviceable crown block system. Perform dimensional, visual and functional inspection of the complete assembly.
Verify sheave rotation, alignment, lubrication, guarding and identification plates.
Conduct proof-load or other specified load testing using a documented procedure.
Certificate of conformity Final inspection report Proof-load test record Manufacturing data book The complete assembly should be evaluated against the contractually specified edition of API Spec 8C or another explicitly selected national or international standard.
Product certification should not be confused with ISO 9001, which certifies a quality-management system rather than the crown block itself.
Approved general arrangement drawing
Design calculations
Inspection and test plan
Nameplate details
Operation and maintenance manual
Spare-parts list
Rated capacity, design temperature, serial identification and service limits must be clearly stated.
All critical parts must be traceable.
Final test results must comply with the approved inspection and test plan.
Global Shipment and Compliance Package Provide the technical, quality and regulatory records required for cross-border acceptance and installation. Review document completeness, translation needs, packing condition, preservation and lifting points.
Confirm that shipping marks and documentation match the equipment identification.
Commercial invoice data Packing list Certificate of origin Final data book Check destination-country import, customs, pressure, lifting, workplace-safety and environmental requirements.
CE, UKCA, ATEX, IECEx or similar markings should only be requested when the supplied scope falls within the relevant legal framework.
Export packing specification
Preservation certificate
Country-of-origin document
English operation manual
Regulatory declaration where applicable
Documents must be consistent in model, serial number, quantity and revision status.
Packaging must protect machined surfaces, bearings and coatings during multimodal transport.
Any destination-specific certificate must be identified before purchase order placement.
Procurement note: Define the applicable standard edition, rated loads, operating environment, inspection hold points, documentation language, traceability level and destination-country requirements in the purchase specification before supplier selection.

Evaluate Total Cost, Logistics, Installation, and After-Sales Support

How to Choose Crown Block Components for Global Procurement?
Evaluate Total Cost, Logistics, Installation, and After-Sales Support

Choosing crown block components for global procurement demands more than comparing quotations. The purchase price is only the visible part. Evaluate sheave dimensions, rated load, bearing design, materials, certificates, and inspection records. These details affect service life and drilling safety. Ask suppliers for test procedures and traceable serial records. A complete technical file supports engineers, auditors, and replacement planning.

Calculate total cost across the component’s expected service period. Include packaging, inland transport, ocean or air freight, insurance, duties, installation tools, and downtime. A compact component may reduce freight costs, but unusual dimensions can require special handling. Confirm crate sizes, lifting points, moisture protection, and delivery terms before ordering. Route planning matters. Spreadsheets can still mislead. A low quotation may become expensive after port congestion, storage delays, or missing customs documents. Even careful forecasts need a contingency allowance.

Installation costs deserve equal attention. Check foundation interfaces, shaft alignment, torque requirements, lifting capacity, and commissioning procedures. Provide illustrated manuals and remote technical guidance for local teams. After-sales support should include critical spares, response targets, inspection advice, and warranty boundaries. Ask how quickly seals, bearings, or sheaves can be supplied. Request training records and escalation contacts. Do not assume every installer has the same equipment or experience. A support package reduces disruption, although it cannot remove every field error. That limitation should remain visible in the procurement plan.

FAQS

What materials are commonly used for crown block sheaves?

Sheaves commonly use forged or cast alloy steel. Material choice should match load, speed, corrosion, and service temperature.

What should be checked on shafts and bearings?

Shafts need verified strength and accurate heat treatment. Bearings must suit expected radial and axial loads.Small differences matter.

Which manufacturing details deserve close inspection?

Check groove profiles, shaft runout, bearing fits, guards, weld controls, and dimensional inspection records.These details affect service reliability.

What documents should a supplier provide?

Request material certificates, inspection plans, test reports, drawings, load ratings, manuals, and traceability records.Each certificate should match a component serial number.

Does certification alone prove component compliance?

No. Confirm the issuing body, certificate scope, inspection date, standard edition, and serial number.Paperwork can mislead.

What inspections should occur before shipment?

An independent inspector may witness dimensional checks, surface examinations, hardness testing, and proof-load testing.Photographs should show calibrated instruments and identification marks.

How can a supplier’s qualifications be evaluated?

Review production capacity, calibration records, corrective-action history, and sample inspection reports.An independent factory audit can reveal mixed materials or poor storage.

What should global buyers verify for destination countries?

Compare supplier documents with destination rules and project specifications.Check conformity declarations, packaging labels, translated manuals, test reports, and traceability records.

How can teams reduce mistakes during international procurement?

Keep a document register linking each component, report, shipment, and inspection result.Pause when requirements conflict.A technical review after the first production sample can expose costly assumptions.

Conclusion

Choosing Crown Block Components for global procurement requires a structured evaluation of technical performance, quality, and supply reliability. Begin by defining the component types, required specifications, load ratings, dimensions, connection methods, and operating conditions. Each component should be assessed for compatibility with the complete drilling or lifting system, including expected loads, speed, temperature, corrosion exposure, maintenance demands, and site conditions.

Material selection, manufacturing consistency, and supplier qualifications are equally important. Buyers should review applicable manufacturing standards, quality management systems, production experience, and technical documentation. Inspection procedures, test reports, traceability records, certifications, and international compliance documents should be verified before purchase. Finally, compare total cost rather than unit price alone, considering packaging, transportation, customs, installation, spare parts, delivery schedules, warranty terms, and after-sales support. A well-defined procurement process helps reduce operational risk, prevent compatibility problems, and secure dependable Crown Block Components for long-term international use.
Charlotte

Charlotte

Charlotte is a seasoned marketing professional with a deep understanding of the company's portfolio and a passion for elevating its presence in the market. With a keen eye for detail and a commitment to excellence, she ensures that our professional blog is regularly updated with insightful articles......