Buying a Crown Block for drilling operations is not a simple equipment purchase. It affects lifting performance, rig compatibility, worker safety, maintenance planning, and project costs across borders. A suitable unit must match the derrick design, drilling load, operating environment, and expected service life.
Global buyers often compare price first. That can be a costly mistake. A low quotation may exclude inspection, spare parts, transport protection, certification, or installation support. Buyers should examine sheave diameter, rated capacity, rope size, bearing condition, frame construction, and manufacturer documentation. Clear technical records matter.
This guide presents seven practical Crown Block buying tips for international purchasers. It focuses on supplier verification, engineering compatibility, quality inspection, compliance documents, logistics, warranty terms, and long-term support. Each area deserves evidence, not promises. Ask for drawings, test reports, serial numbers, maintenance history, and recent inspection results. Small details can reveal larger risks.
Experience also teaches a less comfortable lesson: even a careful checklist can miss site-specific problems. Salt air, dust, extreme temperatures, and limited local service may change the purchase decision. A trusted supplier should answer technical questions directly and explain limitations honestly. Avoid vague claims such as “heavy duty” without measurable data.
The right Crown Block is not always the newest or cheapest option. It is the one that fits the rig, meets recognized safety expectations, and remains supportable after delivery. Careful comparison takes time. Yet rushed buying can create delays, unsafe operation, and expensive replacement work.
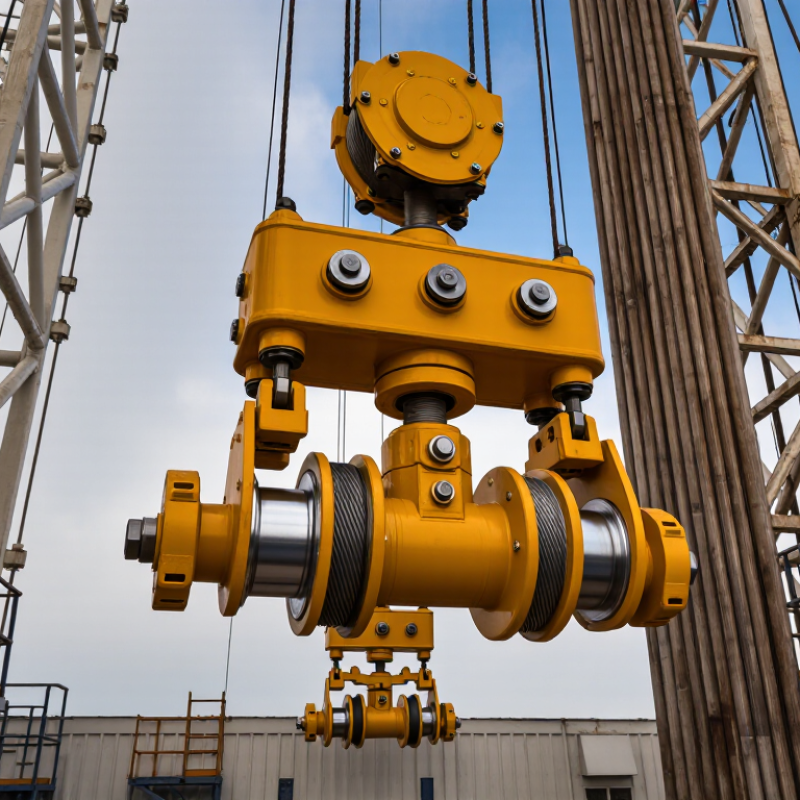
Buying a crown block for a global rig starts with the hook-load envelope. A 250-ton unit may suit a compact land rig, while a 2,000-ton unit demands heavier framing, larger sheaves, and stronger bearings. Do not match capacity by nameplate alone. Check maximum static hook load, traveling-block weight, drilling-line size, reeving arrangement, and expected shock loading. API Spec 8A and API RP 8B require equipment ratings, inspection practices, and traceable documentation. These references should guide the technical review.
Seven checks reduce expensive mistakes: verify the rated load against real rig duty; confirm sheave diameter-to-rope ratio; inspect bearing-life calculations; review fatigue analysis; match crown-block width to the mast; demand load-test certificates; and confirm spare-part availability. API RP 8B emphasizes condition monitoring and inspection intervals, but field history still matters. Ask for records from comparable 250–2,000-ton applications. Paperwork is not performance.
Rig duty changes the answer. A workover unit may lift less often, while a deep-drilling rig cycles heavy loads repeatedly. The 2024 IADC Health, Safety and Environment data continues to show that equipment integrity and lifting practices remain central to drilling risk control. Leave margin for dynamic effects, temperature, corrosion, and future upgrades. I would still challenge one assumption: the largest crown block is not automatically the safest choice. Oversizing can increase mast loads, transport weight, and maintenance demands. Review the complete hoisting system with an independent engineer before purchase.
7 Crown Block Buying Tips for Global Buyers
Verify API Spec 8C Compliance, Traceability, and Design Certification
A crown block should arrive with more than a polished finish and a confident sales claim. Request the exact API Spec 8C certificate for the proposed model, configuration, and rated load. Check its issue date, scope, testing basis, and certifying organization. A factory-wide certificate may not cover your selected assembly.
Ask for a traceability package. It should connect the crown block serial number to material certificates, heat numbers, inspection records, and non-destructive testing reports. Review sheave dimensions, bearing details, rope compatibility, and load-test results. Small gaps matter. One missing link can slow acceptance at the rig site.
Design certification deserves close attention. Require approved drawings, load calculations, design assumptions, and documented safety factors. Confirm that the certified design matches the delivered equipment, including guards, pins, shafts, and lifting points. An independent inspector can witness functional and load testing before shipment. Keep clear records in English and the buyer’s working language when possible.
I have seen buyers focus heavily on price. That approach often creates expensive questions later. Still, documents can contain errors, even when the equipment looks excellent. Compare every identifier carefully, and ask for corrections before payment milestones. Do not accept a certificate that cannot be tied to the crown block in front of you.
| No. | Buying Dimension | What to Verify | Required Evidence | Acceptance Check | Buyer Risk Controlled |
|---|---|---|---|---|---|
| 1 | API Spec 8C Compliance | Confirm that the crown block is designed, manufactured, inspected, and documented against the purchaser-specified edition of API Specification 8C and any applicable local regulations. | Current compliance statement, product data sheet, design basis, inspection and test plan, and a certificate of conformity identifying the exact equipment model. | The certificate, drawings, nameplate, and purchase specification must show consistent model, rated capacity, and design requirements. | Non-compliant equipment, customs or acceptance delays, and unclear contractual responsibility. |
| 2 | Rated Load and Service Conditions | Match the rated static and operating loads, reeving arrangement, line-pull conditions, working environment, temperature range, and duty cycle to the drilling unit and intended service. | Load calculation, reeving diagram, design load cases, operating limits, dimensional drawing, and duty classification or service description. | Verify that the crown block rating is not evaluated in isolation and is compatible with the drawworks, drilling line, traveling block, hook, and mast or derrick structure. | Overloading, accelerated fatigue, incompatible system ratings, and reduced lifting safety. |
| 3 | Sheave and Drilling-Line Compatibility | Check sheave groove profile, pitch diameter, groove dimensions, number of sheaves, rope diameter range, fleet angle, and reeving direction against the selected drilling line. | Approved general arrangement drawing, sheave detail drawing, rope compatibility statement, material specification, and dimensional inspection report. | Confirm that the rope manufacturer’s recommended sheave relationship and the purchaser’s reeving design are satisfied before shipment. | Wire-rope damage, groove wear, heat generation, poor rope tracking, and shortened service life. |
| 4 | Material Certification and Traceability | Require traceability for load-bearing plates, shafts, sheaves, pins, weldments, bearings, and other safety-critical components from incoming material through final assembly. | Material test certificates, heat or batch numbers, component identification records, welding records, welder qualifications, and non-destructive examination reports. | Cross-check certificates against component markings, approved drawings, purchase specifications, and the final manufacturing data book. | Unverifiable materials, difficult failure investigation, rejected documentation, and weak warranty support. |
| 5 | Design Certification and Engineering Review | Obtain an engineering certification confirming that the design calculations, structural analysis, fatigue assessment, bearing selection, and safety factors are appropriate for the stated service. | Signed and dated design dossier, calculation summary, finite-element analysis where applicable, drawing approval record, and certification by a qualified responsible engineer. | The certification should identify the equipment, design loads, applicable standards, assumptions, revision level, and responsible reviewer. | Uncontrolled design changes, insufficient structural margin, and disputes over engineering responsibility. |
| 6 | Inspection, Testing, and Final Acceptance | Define witness and hold points for dimensional inspection, weld examination, shaft and sheave checks, bearing installation, rotation or functional testing, and load testing where required by the agreed specification. | Approved inspection and test plan, calibrated instrument certificates, dimensional report, NDE reports, functional test record, punch list, and release note. | Use an independent inspection body when contractually required, and close all non-conformities before dispatch. | Hidden manufacturing defects, installation rework, delayed commissioning, and unsafe operation. |
| 7 | Documentation, Maintenance, and Global Delivery | Confirm that the equipment can be installed, operated, inspected, maintained, preserved, and transported under the destination country’s requirements and site conditions. | Installation and operation manual, maintenance schedule, lubrication requirements, spare-parts list, lifting and preservation instructions, packing list, and as-built drawings. | Check document language, units, shipping dimensions, lifting points, corrosion protection, export packaging, and consistency between the data book and delivered equipment. | Installation errors, spare-parts shortages, transit damage, regulatory delays, and avoidable downtime. |
7 Crown Block Buying Tips for Global Buyers
Compare 26–72-inch sheave sizes with the rope diameter, rated load, and available derrick space. A larger sheave usually reduces rope bending stress, but it adds weight and transport difficulty. API RP 9B links sheave geometry with wire-rope service life. Do not treat diameter as a standalone upgrade. The IADC Drilling Manual also stresses that hook load, line pull, rope weight, and reeving efficiency must be checked together.
Tip 1: Confirm the maximum rope diameter first. Tip 2: Compare line capacity at the same rope size. Tip 3: Check the crown block’s static and dynamic ratings. Tip 4: Match the block with the drawworks drum. A 26-inch block may suit a compact rig, while a 72-inch model can support heavier rope systems. Yet, the larger option may exceed local lifting limits. That detail is easy to miss.
Tip 5: Compare four-, six-, and eight-part reeving layouts. In a simplified six-part example, 90% efficiency provides about 5.4 effective supporting parts. Real friction can reduce this figure. Tip 6: Review sheave groove wear limits and rope fleet angles. Tip 7: Request certified load charts under API Spec 8A and ISO 13535. Paper capacity is not operating capacity. Field measurements may disagree with old drawings, and that should trigger a second review.
A crown block is a critical lifting component, not merely a steel frame with sheaves. Ask for material certificates, weld procedures, and traceable inspection records. Require non-destructive testing on welds, pins, shafts, and other highly stressed areas. Magnetic particle testing can reveal surface cracks. Ultrasonic testing can identify hidden discontinuities.
Request the NDT method, inspector qualification, equipment calibration, and acceptance criteria. A vague “passed inspection” statement is weak evidence. Require a factory load test witnessed by an independent inspector when practical. Confirm the test load, holding time, deflection readings, and final inspection results. The report should identify the tested unit by serial number.
Do not accept a claimed safety factor without its design basis. Request calculations covering rated load, dynamic effects, fatigue, braking forces, and uneven loading. Verify that the factor applies to the complete assembly, not only one component. Compare the rated capacity with your operating conditions, including temperature, duty cycle, reeving arrangement, and maintenance limits.
I have seen buyers focus on price and overlook documentation gaps. That mistake becomes expensive later. A polished certificate can still hide missing test details. Ask technical questions before payment, and record every answer. Keep drawings, inspection reports, load-test data, manuals, and replacement-part specifications together. Independent review may feel slow, but it can expose assumptions that factory paperwork misses.
Global crown block buying requires more than comparing lifting capacity and price. Shipping can reshape the purchase decision. UNCTAD’s Review of Maritime Transport 2024 reports that over 80% of global merchandise trade by volume moves by sea. Confirm the packed dimensions, gross weight, port options, and delivery terms before signing. A small measurement error can trigger oversized-cargo fees. It happens.
Request corrosion protection for sea transit, moisture indicators, and a documented packing checklist. The World Bank’s Logistics Performance Index 2023 shows major differences in customs efficiency and shipment tracking between economies. Ask for milestone tracking, customs documents, and a named emergency contact. Do not assume every forwarder offers the same visibility.
Spare parts and warranty terms deserve equal attention. Require a two-year critical-parts list, interchangeability details, recommended stock levels, and lead times for bearings, pins, seals, and brake components. The U.S. Department of Energy’s Operations and Maintenance Best Practices guide indicates maintenance can represent 60–70% of lifecycle costs in industrial assets. Therefore, evaluate inspection labor, lubrication, alignment tools, training, and downtime exposure. Warranty coverage should define operating hours, inspection records, corrosion exclusions, response times, and field-repair responsibility. Vague wording creates expensive arguments. A low-cost crown block may still cost more over ten years. Recheck the assumption.
Match capacity to maximum static hook load, traveling-block weight, rope size, reeving, and expected shock loading. A 250-ton unit may suit a compact land rig. A 2,000-ton unit needs heavier framing, larger sheaves, and stronger bearings.
No. Compare the rating with real duty, duty cycles, dynamic effects, temperature, corrosion, and future upgrades. Paperwork is not performance. Field records from similar rigs can reveal practical weaknesses.
A workover rig may lift less frequently. A deep-drilling rig may repeat heavy cycles throughout the day. Review braking forces, fatigue exposure, maintenance limits, and uneven loading.
Confirm the sheave diameter-to-rope ratio and crown-block width. The width must fit the mast without creating alignment problems. Check rope compatibility, sheave details, shafts, pins, and lifting points.
Request approved drawings, load calculations, design assumptions, material certificates, inspection records, and test reports. Each document should identify the supplied unit clearly. A factory-wide certificate may not cover your exact assembly.
Match the serial number with heat numbers, material records, non-destructive testing, and load-test results. Check identifiers carefully. One missing link can delay acceptance at the rig site.
Require qualified non-destructive testing for welds, pins, shafts, and other highly stressed areas. Magnetic particle testing can reveal surface cracks. Ultrasonic testing can identify hidden discontinuities. Request methods, calibration records, inspector qualifications, and acceptance criteria.
It should state the tested serial number, test load, holding time, deflection readings, and final inspection results. An independent inspector should witness testing when practical. A vague “passed inspection” statement is weak evidence.
No. Oversizing can increase mast loads, transport weight, and maintenance demands. The assumption sounds reasonable, but it needs testing. Have an independent engineer review the complete hoisting system before purchase.
Choosing the right Crown Block is essential for safe and efficient drilling operations, especially for global buyers managing demanding rig environments. Start by matching the block’s rated capacity to expected hook loads from 250 to 2,000 tons, while considering duty cycles, operating conditions, and long-term wear. Confirm API Specification 8C compliance, complete material traceability, engineering records, and design certification. Compare sheave sizes from 26 to 72 inches, along with line capacity, groove design, and reeving layouts, to ensure compatibility with the intended drilling system.
Before purchasing, require documented non-destructive testing, factory load testing, inspection reports, and clearly stated safety factors. Buyers should also assess transportation requirements, installation support, spare-parts availability, warranty coverage, and expected maintenance costs. A reliable supplier should provide clear technical documentation and responsive after-sales service across regions. Evaluating the total lifecycle cost—not only the initial purchase price—helps ensure the Crown Block delivers dependable performance, safe operation, and practical value throughout its service life.
MTPM RigParts